
Custom CNC Turning Services
A CNC turning plan brings geometry, critical dimensions, finish and inspection needs together. The drawing, material and quantity provide the basis for a quotation and agreement on the manufacturing process and schedule.









Let's start a new CNC turning project!


Upload Your CAD Files for Fast DFM & Quote
.step.iges.stl.pdf.dwg
Plan Your CNC Turning Project
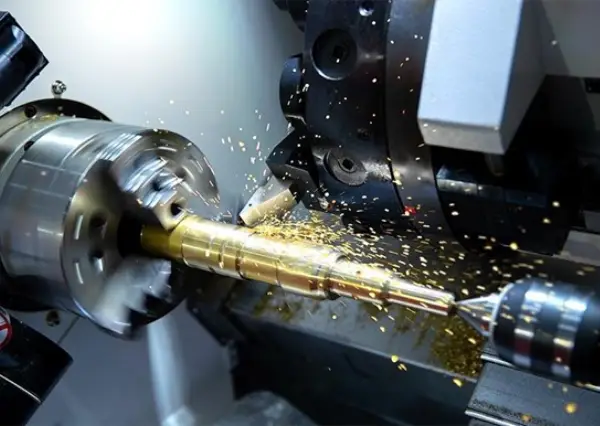
Turning creates rotational features. For a quote, share the geometry, material, quantity and drawings. Review any live-tooling or secondary-milling requirements, fixturing, critical tolerances and inspection needs with LEAD MFG before choosing the production plan.

Rotational Feature Review
External diameters, faces and shoulders are assessed against the drawing, material and workholding.

Diameters and shoulders
Datum and workholding
Critical dimensions
Bores and Grooves
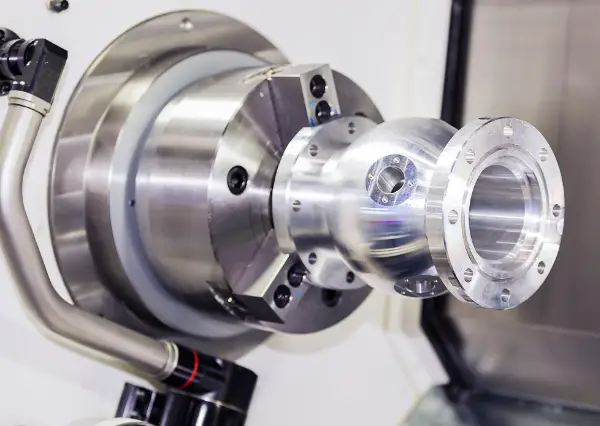
Define internal diameters, depths, grooves and inspection access so tooling and the setup can be reviewed.
Internal features
Groove geometry
Tool access

Threads and Secondary Features
Specify thread standard, size and class. Radial holes or flats require a separate milling review.
Thread specification
Mating and fit
Secondary operations
CNC Turning Parameters
Achievable diameters, lengths, geometric tolerances and threads depend on material, geometry, workholding, operations and inspection. The drawing must identify the critical requirements so values can be assessed for the actual part.
Parameter | Capability | Conditions |
|---|---|---|
Maximum part diameter and length | Ø300 × 400 mm long | Diameter includes turret clearance; longer parts require a second operation or milling review. |
Minimum turned part | Ø1.5 mm; length 1.0 mm | Minimum diameter requires a guide bush and dedicated tooling. |
Part repeatability | ±0.010 mm | Part-to-part reference; drawing tolerances, setup and measurement remain project-specific. |
Roundness / cylindricity | Standard 0.010 mm; best 0.005 mm | Best applies at Ø≤100 mm; do not apply it to all diameters. |
Multi-step concentricity | Standard 0.015 mm; best 0.005 mm | Best requires a single setup; reversing the part can widen the concentricity stack. |
Face runout | Standard 0.010 mm; best 0.005 mm | Datum and workholding conditions must be defined. |
Length tolerance | Standard ±0.050 mm; best ±0.010 mm | Best requires positive face location. |
Tube wall / groove width | 0.5 mm / 0.5 mm | Thin tubes require internal support; geometry and material affect access. |
Threads / slender parts | M1–M30; external 6g / internal 6H | ISO 965 go/no-go checking; L/D>6 needs tailstock or steady-rest support and reduces usable length. |
Surface roughness | Ra 0.8–1.6 µm as-turned; 0.4–0.8 µm fine turned | Ra 0.2 µm requires polishing. The listed lathes are two-axis; radial holes and flats require milling. |
CNC Turning Drawing Checklist
Good part design helps reduce machining risk, control cost, and improve the consistency of CNC turned parts. Use the following guidelines when preparing your drawing or CAD file for custom CNC turning.
Radii
Tool access and mating fits influence the radii, shoulders and fillets that can be planned. Internal and external radii, required fillets and any allowed corner relief need to be defined on the drawing.
Threads and Tapped Holes
Thread feasibility depends on tool access, material and the proposed setup. The thread specification therefore needs its standard, nominal size, pitch, class or fit, engagement length and gauging requirements.
Wall Thickness
Thin-wall review connects wall thickness, unsupported length and critical diameters with deformation risk. Workholding and inspection access must be assessed for the material and geometry.
Marking and Engraving
A marking or engraving request defines content, location and legibility. Its process and effect on the part are reviewed separately.
Holes
Deep or small holes need review of tool access and the machining plan. Hole diameter, depth, position, end condition, tolerances and inspection requirements define that review.
Grooves and Slots
Avoid extremely narrow grooves when possible. Wider features improve tool access and machining stability.
CNC Turning Materials
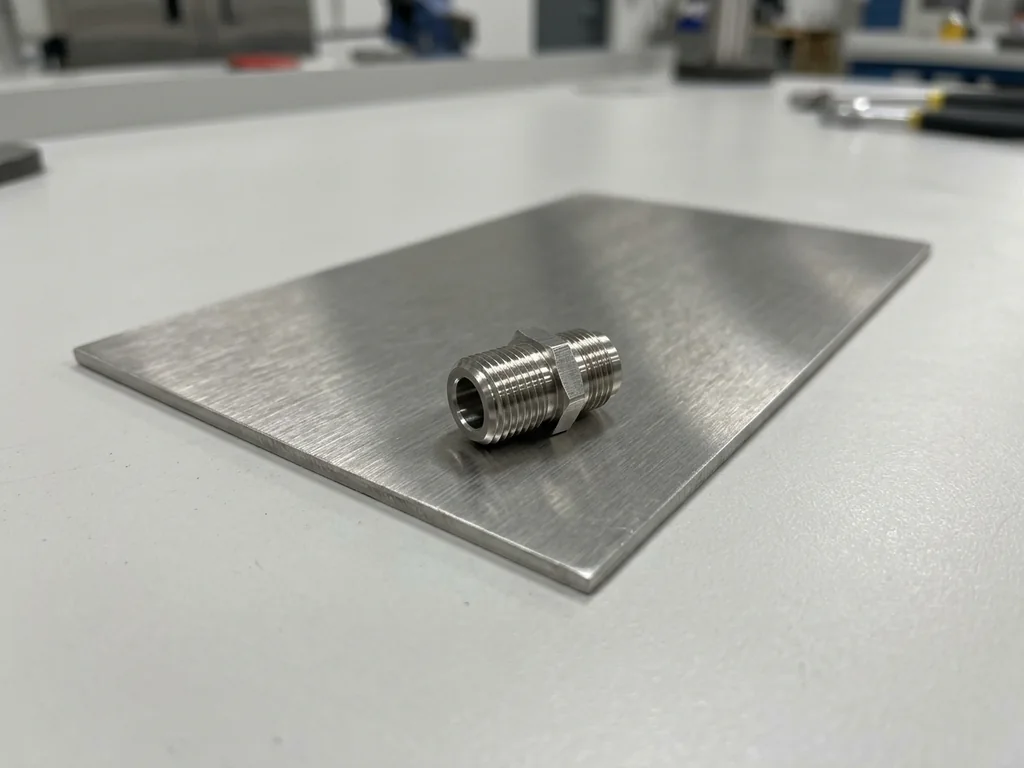
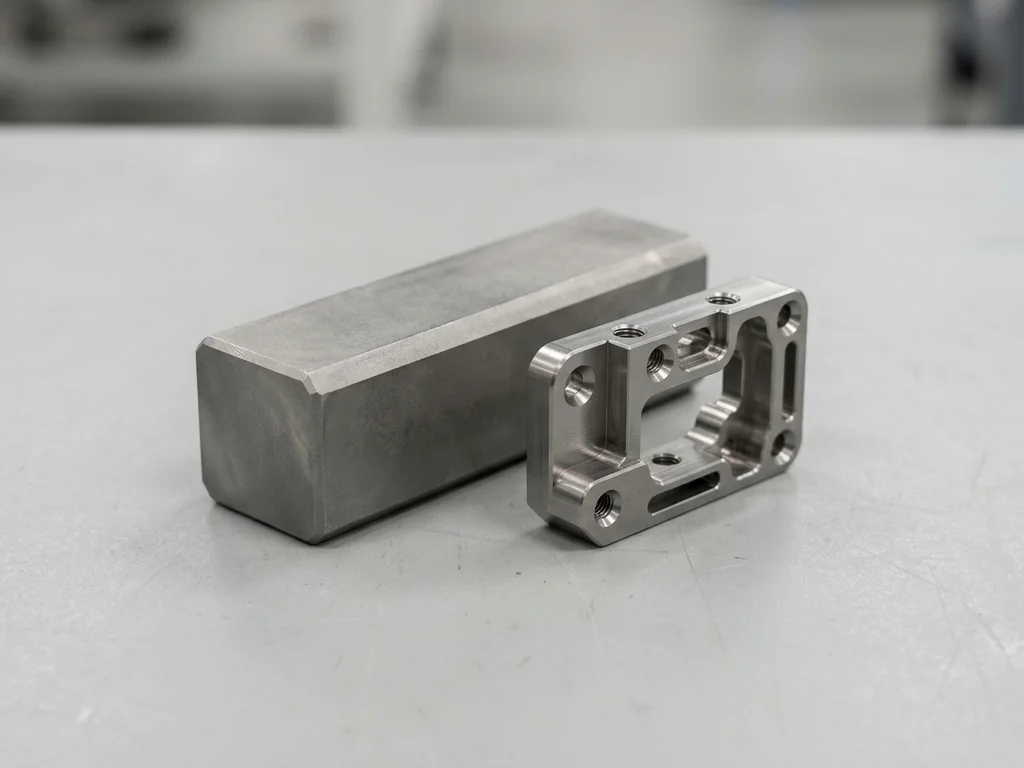
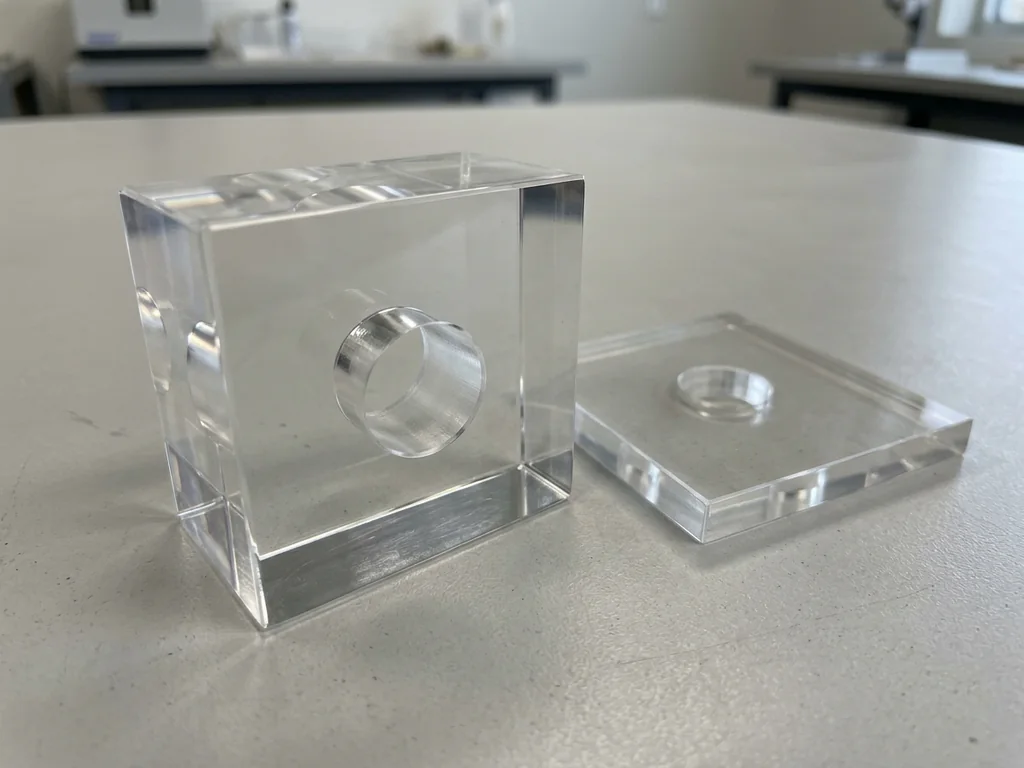
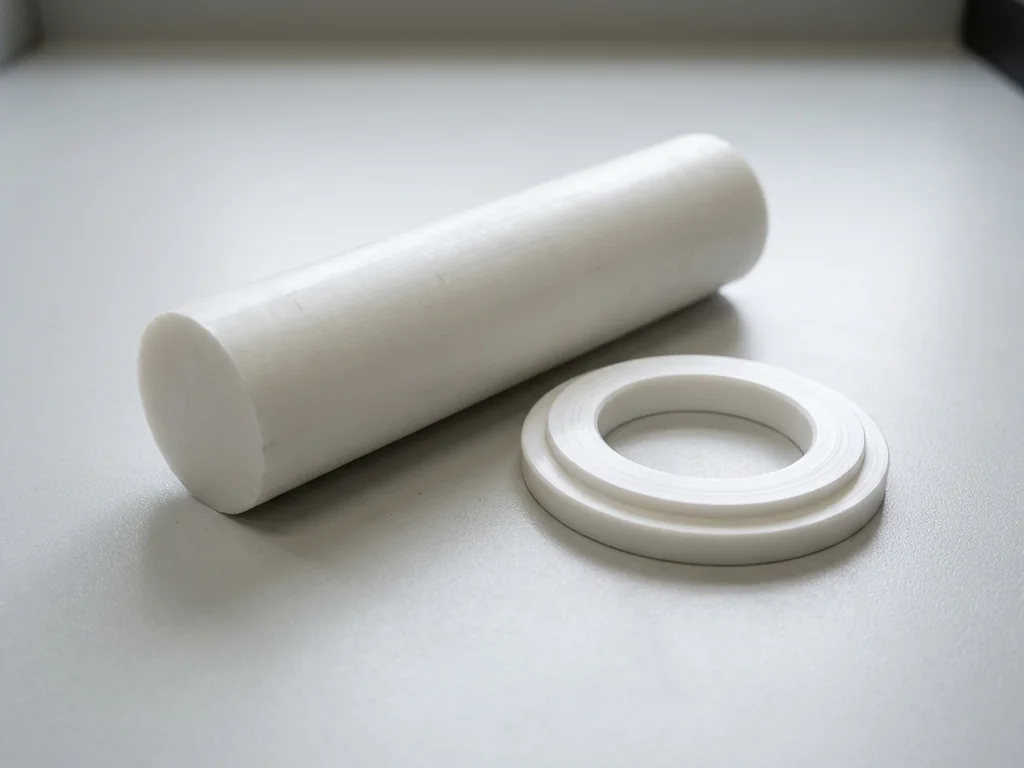
Specify the material grade, standard, stock form and condition. Availability and machining suitability depend on the part, geometry and production requirements.










CNC Turning Surface Finishes
The finish names below are reference options for discussion. Identify substrate, functional surfaces, service environment and dimensional constraints. Availability, masking, appearance and inspection requirements must be assessed with the quotation.

As Machined
As Machined
An as-machined surface retains tool marks from cutting. Specify acceptable texture, cosmetic areas and any surfaces that need further treatment.
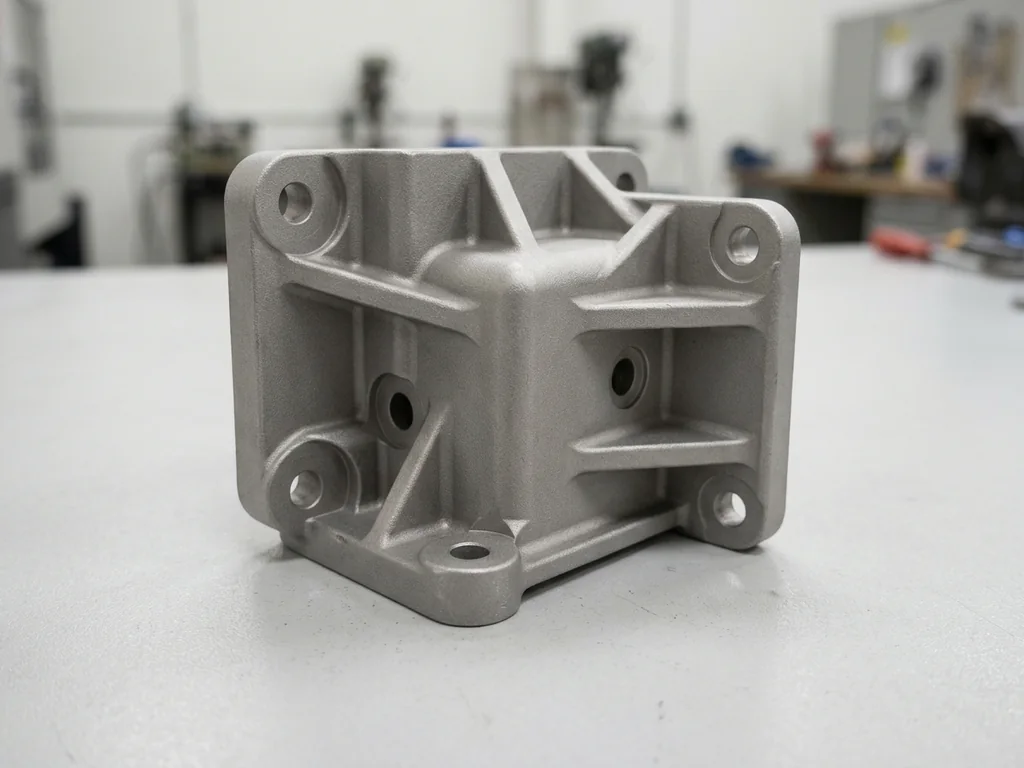
Sand Blasting
Sand Blasting
Blasting uses selected abrasive media to clean or texture surfaces. Specify the finish target, media and areas to protect.
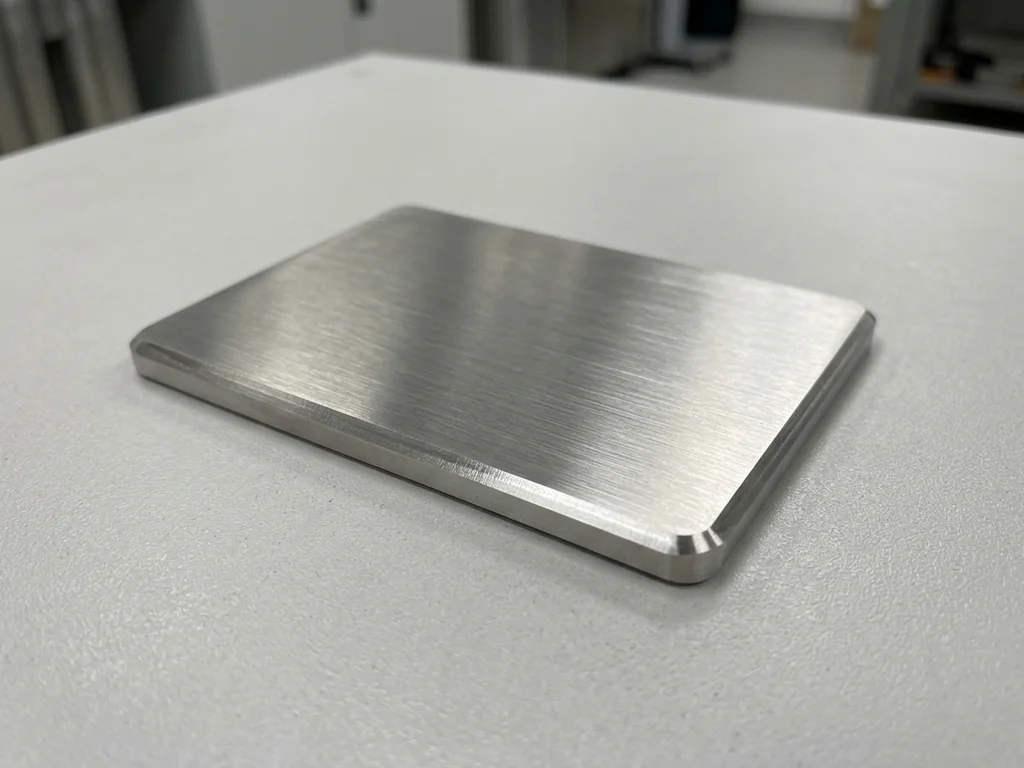
Brushed Finish
Brushed Finish
Brushing creates a directional texture. Specify grain direction, appearance reference, protected surfaces and any dimensional or cleanliness requirements.

Polishing
Polishing
Polishing modifies surface texture and appearance. Specify the target finish, cosmetic areas and critical dimensions; achievable results depend on material and geometry.
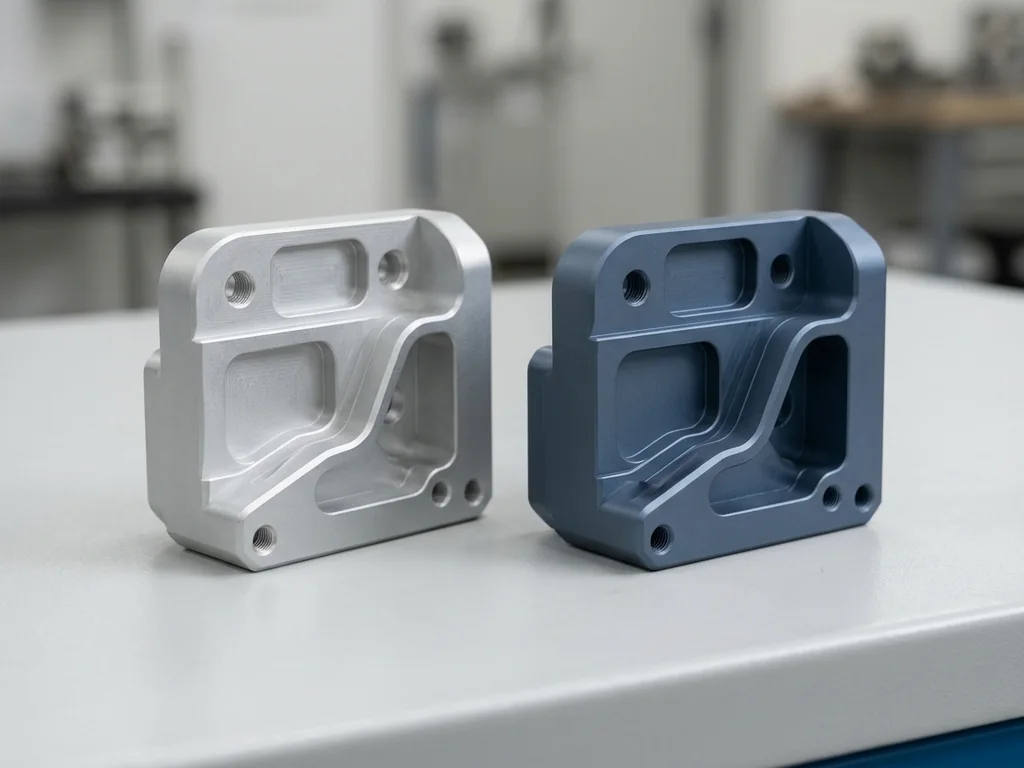
Anodizing
Anodizing
Anodizing forms a surface oxide on suitable substrates. Specify material, coating requirements, color and allowances for critical dimensions before selecting the process.
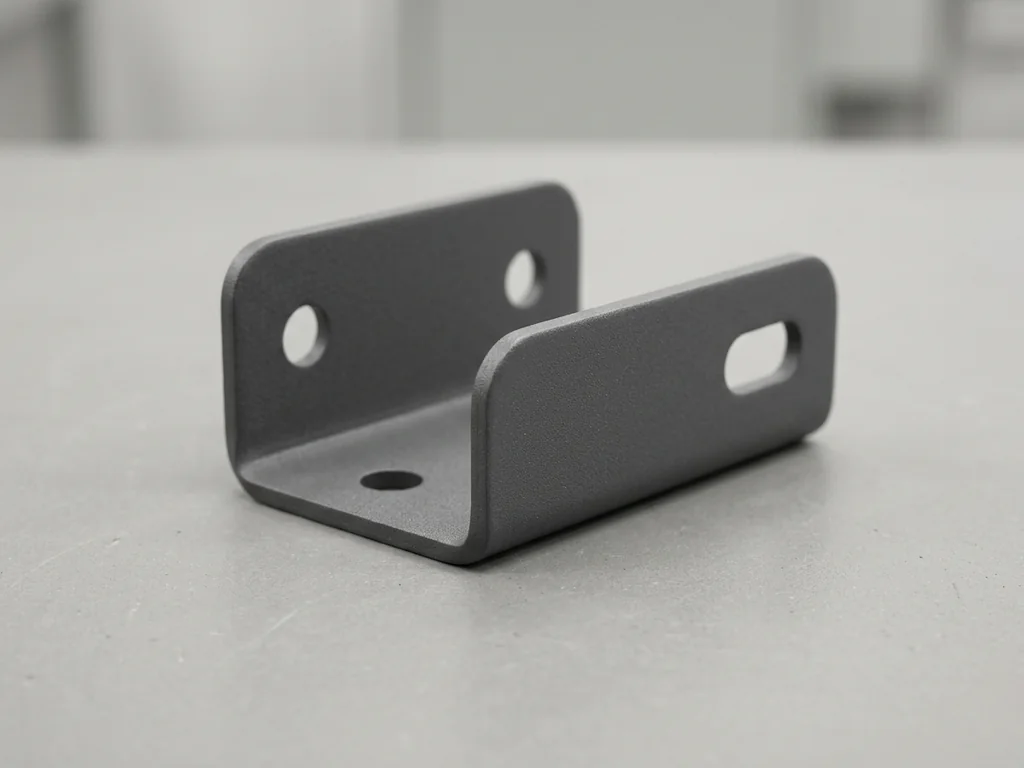
Powder Coating
Powder Coating
A cured powder coating adds a protective or decorative finish. Specify the coating, color, texture and masked areas.
Passivation
Passivation
Passivation treats compatible stainless steel to support its protective surface film. Specify the grade and acceptance requirements.

Electropolishing
Electropolishing
Electrochemical polishing removes surface peaks. Review material removal, critical dimensions and masking for the part.
Other processes to discuss: Tumbling can deburr suitable small parts. Review edge condition, dimensional sensitivity, media and access to recesses before selecting the process. For an aluminum conversion coating, specify the system, standard and chemical restrictions, together with any paint-adhesion or corrosion requirements. Electroplating deposits a metallic layer electrochemically. Specify substrate, coating metal, thickness and critical fits, with corrosion, wear or conductivity targets. Black oxide is a conversion finish for suitable ferrous materials. Specify material, appearance, post-treatment and corrosion requirements for the intended environment. Heat treatment changes properties according to alloy and process. Specify the required condition and consider distortion, dimensional changes and any subsequent machining.


Industry slide guide: 1: Aerospace; 2: Automotive; 3: Automation; 4: Medical Devices; 5: Robotics; 6: Consumer Products.
CNC Turning for Aerospace
Turned shafts, bushings and fittings can be reviewed against the specified alloy, critical features and inspection requirements. Share applicable drawings and documentation needs.
View industryCNC Turning for Automotive
For shafts, sleeves and threaded fittings, define the material, mating features, quantity and inspection requirements before selecting the machining plan.
View industryCNC Turning for Automation
Turned shafts, spacers and rollers can support an equipment assembly. Identify datum surfaces, bearing fits and operating conditions.
View industryCNC Turning for Medical Devices
For turned instrument components, specify the material, surface finish, cleaning and documentation requirements for the intended use.
View industryCNC Turning for Robotics
Review shafts, bushings and bearing interfaces against the assembly datums, loading and critical dimensions.
View industryCNC Turning for Consumer Products
Turned knobs, pins and fittings can be assessed for fit, visible surfaces, material and finish before prototype or production planning.
View industryMore Turning Applications and Part Shapes
Part shapes and application labels help describe a turning request. Operating environment, material, critical fits and inspection criteria determine the review against the drawing and proposed process.
 Electronics
- Communication
- Semiconductor
- New Energy


Frequently asked questions
These answers address turning geometry, materials, tolerances, inspection, cost and production scheduling. Drawings and requirements support a request for DFM feedback and a project-specific quotation.
What parts can CNC turning make?

Turning is commonly used for rotational features on shafts, pins, sleeves, bushings, spacers and similar shapes. Threads, bores, grooves or off-axis features need appropriate tooling and setups. Assess the complete drawing before choosing the manufacturing process.
Can you produce plastic turned parts?
ABS, PC, POM, PA and PTFE are material families that may be discussed for turned parts. Specify grade, stock form, tolerances and service conditions; material availability and machining suitability need project review.
What’s the difference between CNC milling and CNC turning?
In milling, a rotating cutting tool removes material. In turning, the workpiece rotates while tools engage it. The choice depends on features, material, tolerances and setup; some parts need both processes. Compare the complete drawing, inspection needs and quotation when selecting the manufacturing process.
How long does CNC turning take?
For 10–100 parts, typical production is 3–10 business days from quotation confirmation. Quantity, material, geometry and finishing can affect the project schedule. Agree timing in the quotation.
How much does CNC turning cost?
The quote depends on material, stock size, geometry, tolerances, finish, inspection coverage and quantity. Send the 3D design, with a supporting 2D drawing where available, to request a project-specific price.